Why Stainless Steel 316 Suits Marine-Use Sheet Metal Fabrication Parts?
2026-10-15
Marine equipment operates in conditions where salt spray, humidity, temperature changes, and repeated exposure to seawater can accelerate metal corrosion. Selecting the right material is therefore essential when manufacturing Sheet Metal Fabrication Parts for vessel interiors, coastal facilities, offshore equipment, and marine electrical enclosures. Stainless steel 316 is frequently specified for these applications because its molybdenum content improves resistance to chloride-induced pitting and crevice corrosion compared with conventional 304 stainless steel. At Cangzhou Shengsen Metal Products Co., Ltd., we evaluate material selection alongside sheet thickness, forming requirements, weld design, surface finish, and the actual service environment. This approach helps engineers balance corrosion resistance, fabrication quality, structural requirements, and long-term maintenance costs.
What Makes Grade 316 Suitable for Saltwater Environments?
The primary advantage of 316 stainless steel is its ability to resist localized corrosion in many chloride-containing environments. Its chemical composition includes chromium, nickel, and molybdenum. Chromium supports the formation of a passive surface film, nickel helps maintain the austenitic structure, and molybdenum improves resistance to pitting and crevice corrosion.
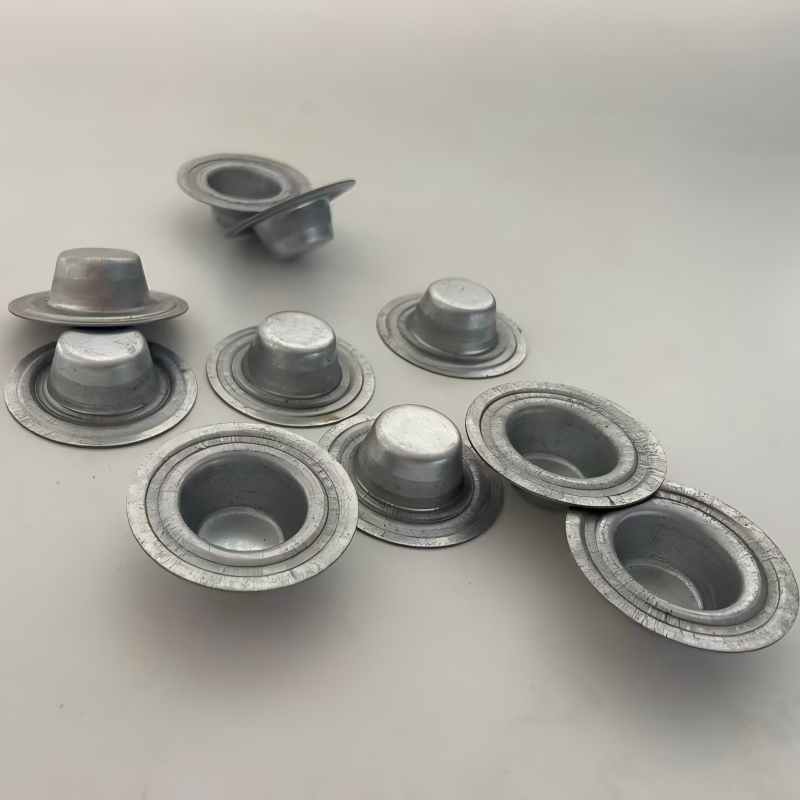
These characteristics make 316 a practical material for marine brackets, equipment covers, mounting plates, protective housings, access panels, and selected structural fittings. However, seawater exposure varies considerably between applications. A sheltered component exposed to occasional salt spray may experience very different corrosion conditions from a continuously immersed fitting or a joint where seawater remains trapped.
Our material selection process distinguishes between general atmospheric exposure, splash-zone conditions, and continuous immersion. Grade 316 performs well in many coastal and marine atmospheric environments, but it is not immune to corrosion in seawater. Stagnant chloride-rich water, deposits, narrow crevices, elevated temperatures, and inadequate maintenance can still cause localized attack.
| Material characteristic | Typical 316 stainless steel | Engineering significance |
| Chromium content | Approximately 16 to 18 percent | Supports passive film formation and general corrosion resistance |
| Nickel content | Approximately 10 to 14 percent | Stabilizes the austenitic microstructure and supports formability |
| Molybdenum content | Approximately 2 to 3 percent | Improves resistance to chloride-induced pitting and crevice corrosion |
| Carbon content | Maximum 0.08 percent for standard 316 under common ASTM specifications | Relevant to welding and sensitization considerations |
| Magnetic behaviour | Generally nonmagnetic in the annealed condition, although forming may induce some magnetism | Useful when magnetic response is part of the design requirement |
| Typical material condition | Solution annealed | Provides a common starting condition for fabrication and corrosion performance |
These figures are typical reference ranges for standard Type 316, not guaranteed values for every supply. The applicable standard, product form, material certificate, and purchase specification determine the actual acceptance limits. Grade 316L, which has a maximum carbon content of 0.03 percent under common specifications, may be preferred for welded assemblies where reduced sensitization risk is important.
How Does 316 Compare with 304 and 316L During Fabrication?
Material selection should account for both corrosion exposure and manufacturing demands. Grade 304 is widely used for general indoor and outdoor fabrication, but its lack of molybdenum makes it less resistant to chloride-induced pitting than 316 under comparable conditions. Grade 316 is often the more appropriate choice when components encounter persistent salt spray or marine humidity.
Grade 316L shares the principal alloying characteristics of 316 but has a lower maximum carbon content. During welding, this can reduce the risk of chromium carbide precipitation at grain boundaries in the heat-affected zone. It does not eliminate every welding-related corrosion risk, so suitable welding procedures, joint design, and post-fabrication cleaning remain important.
| Selection factor | 304 stainless steel | 316 stainless steel | 316L stainless steel |
| Typical corrosion resistance | Good for many general environments | Improved resistance to chloride-related localized corrosion | Similar general alloying benefits to 316, with lower carbon |
| Molybdenum addition | Normally absent as a deliberate major alloying addition | Approximately 2 to 3 percent | Approximately 2 to 3 percent |
| Welding considerations | Requires appropriate procedures and post-weld care | Requires control of heat input and weld cleanliness | Often preferred for welded assemblies where low carbon is beneficial |
| Forming performance | Good for many sheet metal processes | Good formability, with work hardening during deformation | Generally similar to 316 for common fabrication operations |
| Typical marine suitability | Conditional on exposure and maintenance | Suitable for many marine atmospheric and splash-exposed applications | Useful for marine fabrications involving substantial welding |
For a welded enclosure installed on a coastal vessel, 316L may offer a useful combination of chloride resistance and reduced sensitization risk. For a formed bracket with limited welding, standard 316 may be adequate when its material certificate and processing requirements meet the design specification. Neither grade should be selected solely by assuming that lower carbon automatically makes it more resistant to all forms of seawater corrosion.
At Cangzhou Shengsen Metal Products Co., Ltd., we consider the fabrication route before confirming a material recommendation. Laser cutting, punching, bending, forming, and welding can affect dimensional accuracy, residual stress, and surface condition. The final specification should reflect the component drawing and service environment rather than material grade alone.
Which Product Parameters Matter for Marine Sheet Metal Components?
For marine equipment, specifying the alloy without defining the finished component is incomplete. Thickness, dimensions, tolerance, hole positions, bend radii, weld locations, and surface treatment all influence structural performance and corrosion behaviour. Our engineering review starts with the drawing and the component's intended function, then identifies the parameters that need to be controlled during production and inspection.
- Material grade: Specify Type 316 or 316L according to the relevant ASTM, EN, or other agreed material standard. Confirm the designation on the material certificate.
- Sheet thickness: Select thickness according to design loads, unsupported spans, vibration, impact exposure, and allowable deflection. There is no universal thickness for all marine components.
- Dimensional tolerance: Define overall dimensions, hole diameters, hole-to-edge distances, flatness, and positional tolerances on the approved drawing.
- Bend geometry: Confirm bend angles, inside radii, flange lengths, and forming allowances according to the material condition and tooling.
- Weld requirements: Identify weld type, joint geometry, inspection level, and any applicable procedure qualification requirements.
- Surface finish: Specify the required finish, removal of heat tint, and cleaning or passivation requirements where applicable.
- Inspection documentation: Identify material traceability, dimensional inspection records, and any required weld or corrosion-related acceptance criteria.
Sheet thickness must be evaluated against both mechanical loading and corrosion allowance where the design standard requires one. Although 316 resists many forms of corrosion better than 304, a thin component can still lose functional integrity if exposed to severe localized attack or if its dimensions are unsuitable for the applied load. Structural calculations should account for fasteners, vibration, support spacing, and service conditions.
For dimensional control, our factory uses the approved engineering drawing and agreed inspection criteria as the basis for acceptance. Critical features may include mounting-hole locations, flatness of mating surfaces, and the angle of formed flanges. These details can affect installation, load distribution, sealing, and the fit of adjoining components.
Surface condition is equally important. Iron contamination from carbon-steel tooling, embedded particles, rough weld areas, and retained heat tint can undermine corrosion performance. Fabrication procedures should prevent cross-contamination, while suitable finishing and cleaning processes help restore a clean surface. Passivation can improve the condition of the passive film, but it cannot compensate for poor design, trapped seawater, or unsuitable alloy selection.
How Can Fabrication Design Reduce Corrosion and Maintenance Risks?
Good marine design reduces the conditions that allow corrosive deposits and seawater to accumulate. Even a suitable alloy can develop localized corrosion when salt deposits remain wet or when narrow gaps restrict oxygen exchange. Component geometry and installation details therefore deserve the same attention as material chemistry.
Where possible, design panels and brackets to drain freely rather than creating pockets that retain seawater. Avoid unnecessary crevices around overlapping plates, washers, and bolted joints. Where a joint cannot be eliminated, evaluate suitable sealing, drainage, cleaning access, and inspection requirements. These measures are especially important near fasteners and gasket interfaces.
Welding also requires a controlled process. Excessive heat input, unsuitable filler selection, poor shielding, and incomplete removal of heat tint can reduce the corrosion performance of the finished assembly. Use a qualified welding procedure appropriate to the thickness, joint configuration, and applicable code. After welding, remove contamination and heat tint using an appropriate method, then perform cleaning and passivation where specified.
Our fabrication planning considers the sequence of cutting, forming, welding, finishing, and final inspection. Planning the sequence carefully can reduce rework, protect finished surfaces, and improve dimensional consistency. For marine electrical cabinets, equipment covers, and mounting assemblies, the enclosure design should also account for ingress protection, drainage, ventilation, and galvanic compatibility with connected hardware.
Galvanic corrosion deserves particular attention when stainless steel is electrically connected to dissimilar metals in the presence of an electrolyte. The risk depends on the materials involved, their relative exposed areas, electrical contact, and the availability of seawater. Appropriate isolation washers, compatible fasteners, coatings, and joint design may be necessary. Stainless steel 316 does not remove the need to assess these interfaces.
Maintenance planning should reflect actual exposure. Periodic freshwater washing can remove salt deposits from many marine atmospheric installations, while inspections can identify staining, crevice attack, damaged finishes, and loose fasteners before they become more serious problems. Components in splash zones or harsh chemical environments may require more frequent inspection than equipment installed in sheltered locations.
Frequently Asked Questions About 316 Stainless Steel for Marine Fabrication
Why is 316 stainless steel generally preferred over 304 for marine sheet metal components?
Grade 316 contains approximately 2 to 3 percent molybdenum, which improves resistance to chloride-induced pitting and crevice corrosion compared with 304 under comparable conditions. This makes it a common choice for coastal equipment, marine enclosures, brackets, and fittings exposed to salt spray. However, 316 is not immune to seawater corrosion, particularly in stagnant chloride-rich conditions or tight crevices, so component design, cleaning, and the actual exposure level must be considered.
Should marine sheet metal assemblies use 316 or 316L when welding is required?
Both grades can be welded using suitable procedures, but 316L has a lower maximum carbon content, generally 0.03 percent compared with 0.08 percent for standard 316 under common specifications. This reduces the risk of sensitization associated with chromium carbide precipitation during welding. The final choice should also consider the material certificate, thickness, welding procedure, service temperature, and corrosion exposure. Proper removal of heat tint and post-weld cleaning remain important for either grade.
Can 316 stainless steel be used for components continuously immersed in seawater?
It can be used in some marine systems, but continuous immersion requires a more careful corrosion assessment than ordinary salt-spray exposure. Stagnant seawater, deposits, crevices, elevated temperatures, and biological fouling can increase localized corrosion risk. For critical immersed components, engineers should evaluate the applicable design standard, inspection and maintenance plan, and alternatives such as more highly alloyed stainless steels, duplex grades, or other marine-qualified materials. The choice should be based on the complete operating environment rather than the stainless designation alone.
How Should You Specify Marine-Grade Sheet Metal Components?
Stainless steel 316 is a strong candidate for many marine sheet metal applications because molybdenum improves resistance to chloride-related localized corrosion while the austenitic structure supports practical forming and fabrication. Reliable results still depend on selecting the correct grade, defining thickness and tolerances, controlling welding and finishing, and designing joints that do not trap seawater.
Cangzhou Shengsen Metal Products Co., Ltd. works with customers to evaluate drawings, material requirements, fabrication details, and inspection expectations for custom marine components. Share your component drawings, material grade, sheet thickness, dimensional tolerances, surface finish, and operating environment with our team to discuss a suitable manufacturing specification and request a quotation for your application.