Can Wear Resistant Hot Rolled Heavy Steel Plate Structural Be Welded Without Losing Its Wear Properties
2026-10-21
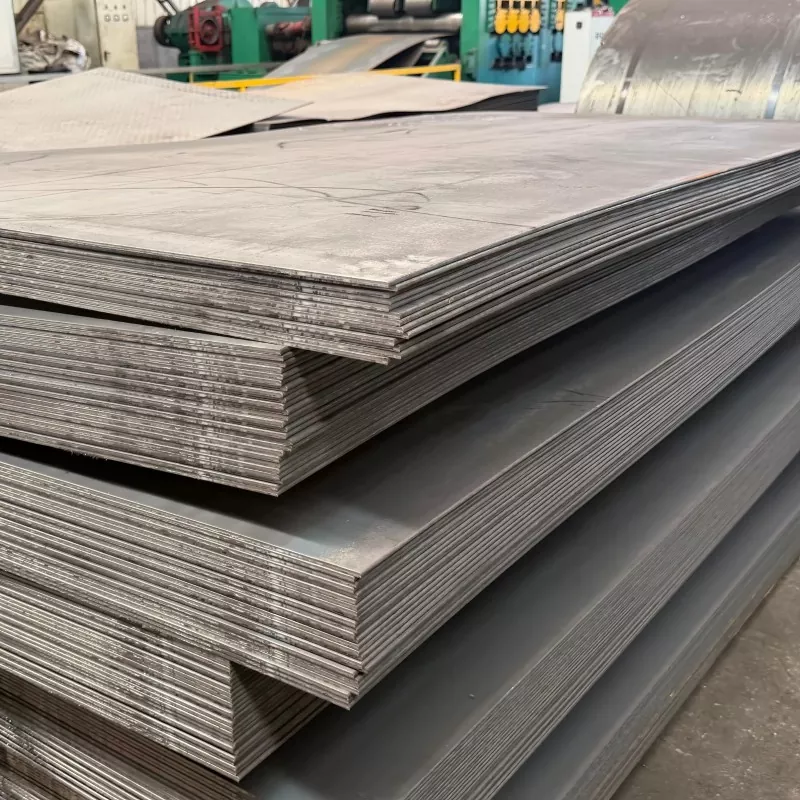
Wear Resistant Hot Rolled Heavy Steel Plate Structural is widely specified for chutes, hoppers, dump truck bodies, and crusher liners, yet fabrication teams often ask whether welding compromises its abrasion resistance. At Sanhe, we supply quenched-and-tempered wear plate with controlled hardness and clean steel chemistry, and we support customers through the welding decisions that determine whether the plate performs as designed in service. The answer is yes—welding can be performed without sacrificing wear properties, provided the heat input, filler selection, and joint design are managed correctly.
Why Welding Affects Wear Performance
Wear resistance in Wear Resistant Hot Rolled Heavy Steel Plate Structural comes primarily from its martensitic or bainitic microstructure and typical Brinell hardness of 400–500 HBW. Excessive heat input creates a softened heat-affected zone (HAZ), reduces hardness, and can trigger hydrogen-assisted cracking in thick sections. Controlled welding preserves the base plate hardness while producing sound joints.
Key Welding Parameters
| Parameter | Recommended Practice | Reason |
|---|---|---|
| Heat input | 0.5–1.5 kJ/mm | Limits HAZ softening |
| Preheating | 100–150 °C for plate over 20 mm | Prevents cold cracking |
| Interpass temperature | Max. 250 °C | Protects tempering |
| Filler metal | Low-hydrogen, matching strength | Avoids hydrogen cracking |
| Joint preparation | Butt joints, avoid excessive bevel | Reduces dilution |
| Post-weld | Slow cooling, no rapid quenching | Maintains toughness |
Practical Steps to Protect Wear Properties
-
Use low-hydrogen consumables and keep them dry; moisture is the leading cause of delayed cracking.
-
Restrict weave width to 3× electrode diameter and avoid excessive passes on the wear face.
-
Place weld seams away from the highest-abrasion zone where possible.
-
For Wear Resistant Hot Rolled Heavy Steel Plate Structural thicker than 40 mm, apply controlled preheat and monitor interpass temperature with a contact thermometer.
-
Never air-cool rapidly after welding; allow slow cooling under insulation for heavy sections.
Sanhe Quality Support
Sanhe provides mill test certificates, hardness mapping, and welding procedure guidance for every heat of Wear Resistant Hot Rolled Heavy Steel Plate Structural. Our technical team reviews joint designs and consumable choices before fabrication, reducing rework and field failures.
FAQ
Q: Does welding reduce the hardness of Wear Resistant Hot Rolled Heavy Steel Plate Structural?
A: Yes, some softening occurs in the heat-affected zone, typically 10–30 HBW below base metal when heat input is controlled within 0.5–1.5 kJ/mm; keeping preheat and interpass temperatures within recommended limits minimizes this drop and preserves abrasion resistance in service.
Q: Which welding process is best for Wear Resistant Hot Rolled Heavy Steel Plate Structural?
A: Gas metal arc welding (GMAW) and shielded metal arc welding (SMAW) with low-hydrogen consumables are most common; submerged arc welding is suitable for long straight seams when heat input is capped, while flux-cored arc welding offers good productivity for thick sections provided hydrogen control is maintained.
Q: Can Wear Resistant Hot Rolled Heavy Steel Plate Structural be welded without preheating?
A: Preheating is not always mandatory for thin plate under 12 mm in mild ambient conditions, but for thickness above 20 mm or low-temperature environments, preheating to 100–150 °C is strongly recommended to prevent hydrogen cracking and to stabilize the heat-affected zone.
Q: How should I prepare the joint before welding Wear Resistant Hot Rolled Heavy Steel Plate Structural?
A: Clean the joint faces to bare metal, remove scale and moisture, use a moderate bevel angle, and avoid excessive root gaps; proper fit-up reduces dilution and heat input, which directly protects the wear face and lowers cracking risk.
For welding procedure recommendations, hardness data, and quotations on Wear Resistant Hot Rolled Heavy Steel Plate Structural, contact Sanhe today—our engineers will help you specify the right grade and fabrication method for your application.